Description
AL 822 aluminum brazing rod — joins aluminum to aluminum or copper
A low-temperature, flux-cored aluminum brazing alloy that joins aluminum to aluminum and aluminum to copper with an ordinary open-air torch. The non-corrosive flux is built into the rod — no separate fluxing, and no cleanup after brazing — which makes it a go-to for HVAC/R coil and line repairs. Fifty rods, bulk-packaged.
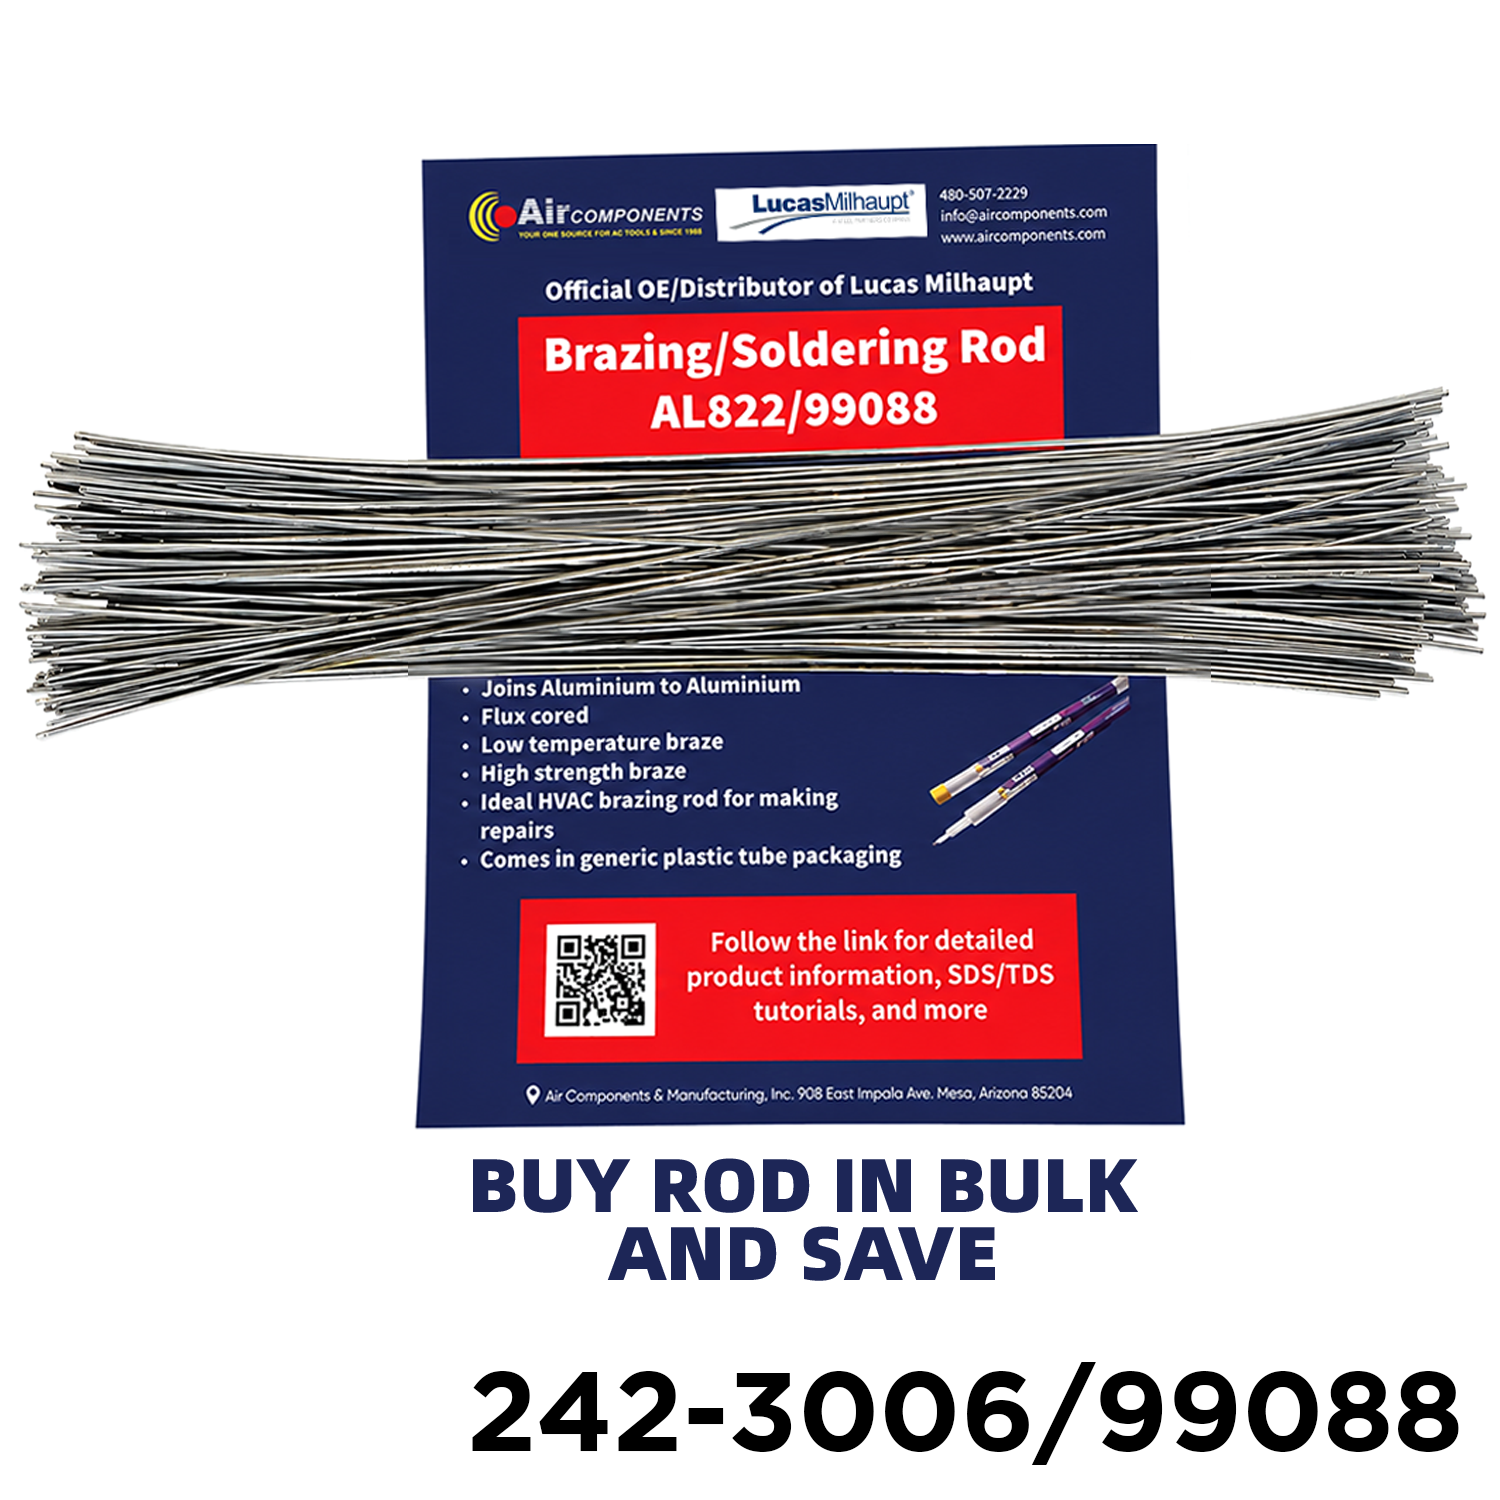
Available in six pack sizes
This listing is the 50-pack (bulk). Need a different quantity?
Easy, strong aluminum repairs
Joins Al & Cu
Braze aluminum to aluminum and aluminum to copper — perfect for mixed-metal HVAC/R and automotive joints.
Flux is built in
Flux-cored with a non-corrosive flux, so there’s no separate fluxing step and no residue to clean off afterward.
Low-temperature
Flows at low braze temperatures (melts around 800°F), so you’re less likely to overheat and warp thin base metal.
High-strength joint
Forms a durable, high-strength braze — shear strengths can exceed 18,000 PSI at the correct joint clearance.
Open-air torch
Designed for open-air heating with a MAPP or propane torch — no special equipment or shielding gas.
HVAC/R staple
Fast, reliable field repairs on coils, lines, and fittings — easy enough for everyday shop use.
Comparable to popular aluminum brazing rods from Alumaloy, Blue Demon, Burnsomatic, and Saker.
AL 822 on the bench
Key numbers
Braze in four steps
Prep the joint
Clean both surfaces and fit the parts to a 0.003–0.005″ joint clearance for the best capillary flow.
Heat the base metal
Use an open-air MAPP or propane torch and heat the parts — not the rod — evenly to braze temperature.
Flow the rod
Touch the flux-cored rod to the heated joint; the built-in non-corrosive flux pulls the alloy into the joint.
Cool & check
Let it cool — no flux cleanup needed. Pressure-test any refrigerant joint before returning to service.
Braze safely. Brazing produces fumes and requires open flame. Work in a well-ventilated area, follow ANSI Z49.1 and the product SDS, and use appropriate PPE. Refer to the SDS for full alloy composition and handling.
Technical details
Note: supplied in generic plastic tube packaging.
You’ll need heat
AL 822 brazes with an open-air torch. Grab a torch to go with it — and the aluminum-only rod for pure aluminum work.
MAPP / propane torch
A self-igniting MAPP or propane torch is all you need to bring the joint up to braze temperature.
Shop the torch →Torch with 5′ hose
The hose-fed version reaches into tight spots and awkward angles on a coil or under a dash.
Shop the hose torch →AL 718 rod
For aluminum-to-aluminum-only repairs, the AL 718 rod is the companion alloy — available in multi-packs.
Shop AL 718 →AL 822 brazing rod FAQ
What metals will AL 822 join?
Do I need separate flux?
What heat source do I use?
How strong is the joint?
AL 822 vs AL 718 — what’s the difference?
Shop welding & brazing supplies
Browse brazing rod, flux, and torches and set your quantities in one place.
Add AL 822 to your order
In stock and ready to ship. Building a brazing kit or need bulk quantities? Call and we’ll set you up.
Add to cart ↑ Contact usHANDY ONE® and Lucas-Milhaupt® are trademarks of their respective owner; other brand names are referenced for comparison and identification only and do not imply affiliation or endorsement. Brazing involves open flame and fumes — follow ANSI Z49.1, the product SDS, and all applicable safety practices. Confirm suitability for your application before use.


